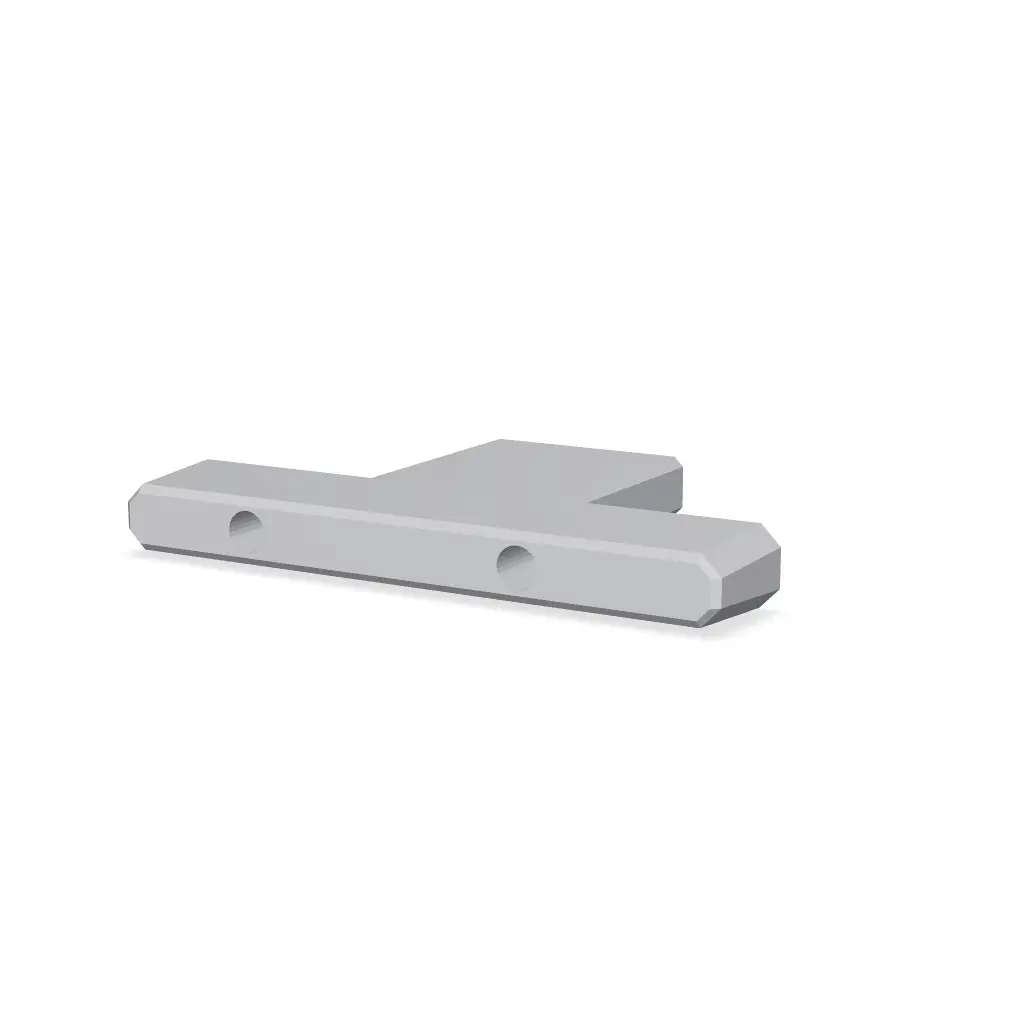
Mast Adapter Forged CF Axis Mast GY fuselage
por Charming Lime en Thangs
Forged carbon fiber mold for adapting AliExpress Axis clone fuselages to genuine Axis 19mm masts. GY fuselages use a 3-degree tapered tenon joint.
Thangs entrega los archivos a usuarios con cuenta gratuita
Licencia
Solo uso personalCC BY-NC-SA 4.0 — Atribución, no comercial, compartir igual
Uso personal dando crédito; sin fines comerciales y las modificaciones con la misma licencia.
Al descargar aceptas respetar la licencia y dar crédito a Charming Lime.
Archivos (12)
- chamfer guage.stl STL · 2 KB
- drill guide base.stl STL · 53 KB
- drill guide cap.stl STL · 77 KB
- front profile.stl STL · 20 KB
- GY Doodadv5.stl STL · 22 KB
- Mold Piston cap.stl STL · 68 KB
- Mold Piston part 1.stl STL · 30 KB
- Mold Piston part 2.stl STL · 46 KB
- side profile.stl STL · 9 KB
- Cavity 1.stl STL · 61 KB
- Cavity 2.stl STL · 55 KB
- cavity 3.stl STL · 54 KB
- Categoría
- Jardín
- Formatos
- STL
- Descargas
- 0
- Publicado
Sobre este modelo
Forged carbon fiber mold for adapting AliExpress Axis clone fuselages to genuine Axis 19mm masts. GY fuselages use a 3-degree tapered tenon joint.
Print the Doodad by itself first to ensure it fits and [the] holes line up. It might need a very light sanding depending on printer quality/pressure advance settings.
An impact drill makes short work of any bolts that might be stuck with epoxy. The mold should be printed at 0.10 mm layer height, 4+ walls, 40% infill, and 20 top and bottom solid layers. Orient the parts as shown in the screenshot. I recommend cubic infill for compression strength. Do NOT use rectilinear, as there is too little compression strength.
Sand all parts of the mold to 220 grit, making sure layer lines are eliminated. It doesn't need to be perfectly smooth, but all the layer lines should be gone, as well as most of the pattern on the top/bottom layers. Go easy where the mold seams join together, and heavier on the side walls of the mold piston[ otherwise, the piston will be too tight. You can use packing tape trimmed to size on the mold clamping surfaces for some extra clearance and easier separation. Spray all sides of the mold/piston parts with mold release before assembling. I used silicone based release.
This requires various M3 hardware and M3x4 D5 (Voron standard) heat-set inserts for the mold piston, and M6 hardware to hold the mold together.
Easy Composites has many good videos on how to make forged carbon.
The mold volume is 79.5cm^3. 67g of 1/2 chopped CF for 60% by weight. 110g of epoxy (this ensures plenty of epoxy to completely wet out the CF)
With TotalBoat High Performance slow hardener, I did not have enough time to paint layers of epoxy and CF using a brush before the epoxy gelled and blew out the mold while compressing it.
I recommend the "dough" method for wetting out the CF: mixing the CF and resin on a plastic sheet with spreaders and then gloved hands, painting the mold and piston with epoxy to prevent pinholes on the surface, and then pressing the dough into the mold before clamping.
The component is slightly hard to demold; go slow, and remove the mold piston plate first. Then use a 2-inch putty knife to free the two mold "ears" first, and then work on the last mold base. Last should be the mold piston part 1, then part 2. The part will need to be sanded to fit; you should only need 220 grit. The only part I used 120 grit for was flattening the tab that is inserted into the mast. Wear a respirator when sanding. Included are some gauges, but the final sand should be to the fuselage and mast.
Drill with a drill press using the guide included; don't try [to] use a hand drill.
Wet sanding through 1500 or 2000 grit gives a nice finish.
tags: hydrofoil, foiling, wingfoil, surf-foil, efoil, kitefoil, axis-foils, axis-doodad, gy-fuselage, mast-adapter, foil-mast, foil-fuselage, foil-parts, aliexpress-foil, forged-carbon, carbon-fiber, composite-mold, epoxy-casting, resin-mold, diy-carbon, mold-making, 3d-printed-mold, functional-print, diy-adapter
Descripción original del autor, publicada en Thangs.