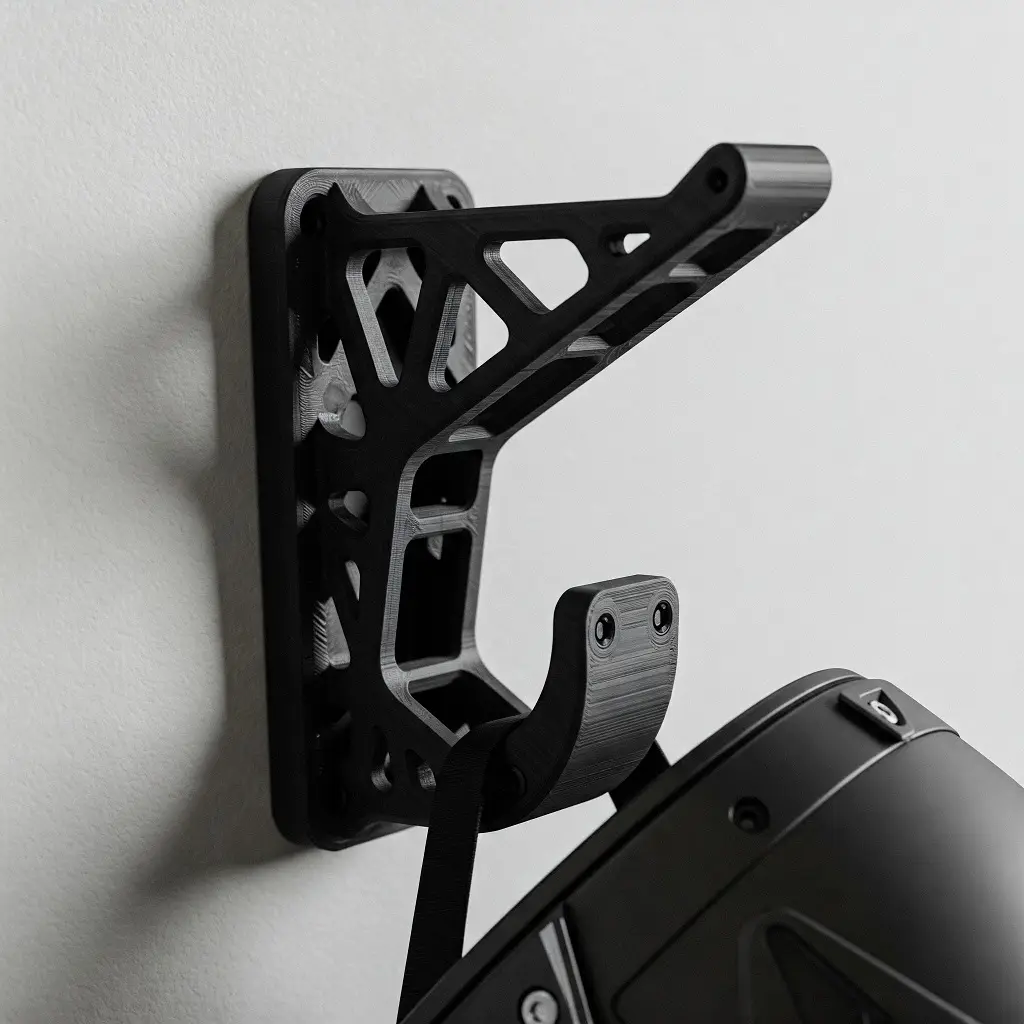
Hook
por AZ 3D Makers en Printables
Designed for style and strength, it's perfect for hanging coats, bags, towels, or keys, helmet etc.
Licencia
Solo uso personalCC BY-NC-ND 4.0 — Atribución, no comercial, sin derivadas
Solo para uso personal, sin modificarlo y dando crédito. No se permite vender ni redistribuir cambios.
Al descargar aceptas respetar la licencia y dar crédito a AZ 3D Makers.
Archivos (1)
- Categoría
- Hogar
- Formatos
- STL
- Descargas
- 2,720
- Publicado
Sobre este modelo
🛠 Cura slicer Settings for Strong PETG Prints
Printer & Material Basics Nozzle Temp: 240–250 °C (start at 245 °C and adjust if needed) Bed Temp: 75–85 °C Cooling Fan: Off or max 20% (layer fan can weaken layer adhesion) Enclosure: Recommended for consistent temps (not mandatory for PETG, but helps)
Layer & Wall Settings Layer Height: 0.2 mm (or 0.28 mm for stronger/thicker layers) Wall Line Count: 3 Wall Thickness: At least 2 – 3 mm Top/Bottom Layers: 5–6 Top/Bottom Thickness: 1.6–2.5 mm
Infill Infill Density: 90 - 100%
Print Speed Print Speed: 30–45 mm/s (slower = stronger) Wall Speed: 25–30 mm/s Initial Layer Speed: 15–20 mm/s Other Key Settings Initial Layer Height: 0.24 mm (good bed adhesion) Z Hop When Retracted: On Retraction Speed: 25–35 mm/s
Generate support : Enable Support structure : Tree
🔧 Pro Tips: Dry your filament – PETG absorbs moisture and it greatly reduces strength. Use a brim or raft if warping is an issue. For critical strength parts: consider increasing wall count and infill rather than relying on 100% infill alone. Turn off "Print Cooling" or keep it minimal for layer bonding.
Descripción original del autor, publicada en Printables.