Bench-Car – Rolling 3D Printer Benchmark
por JAV3D en Printables
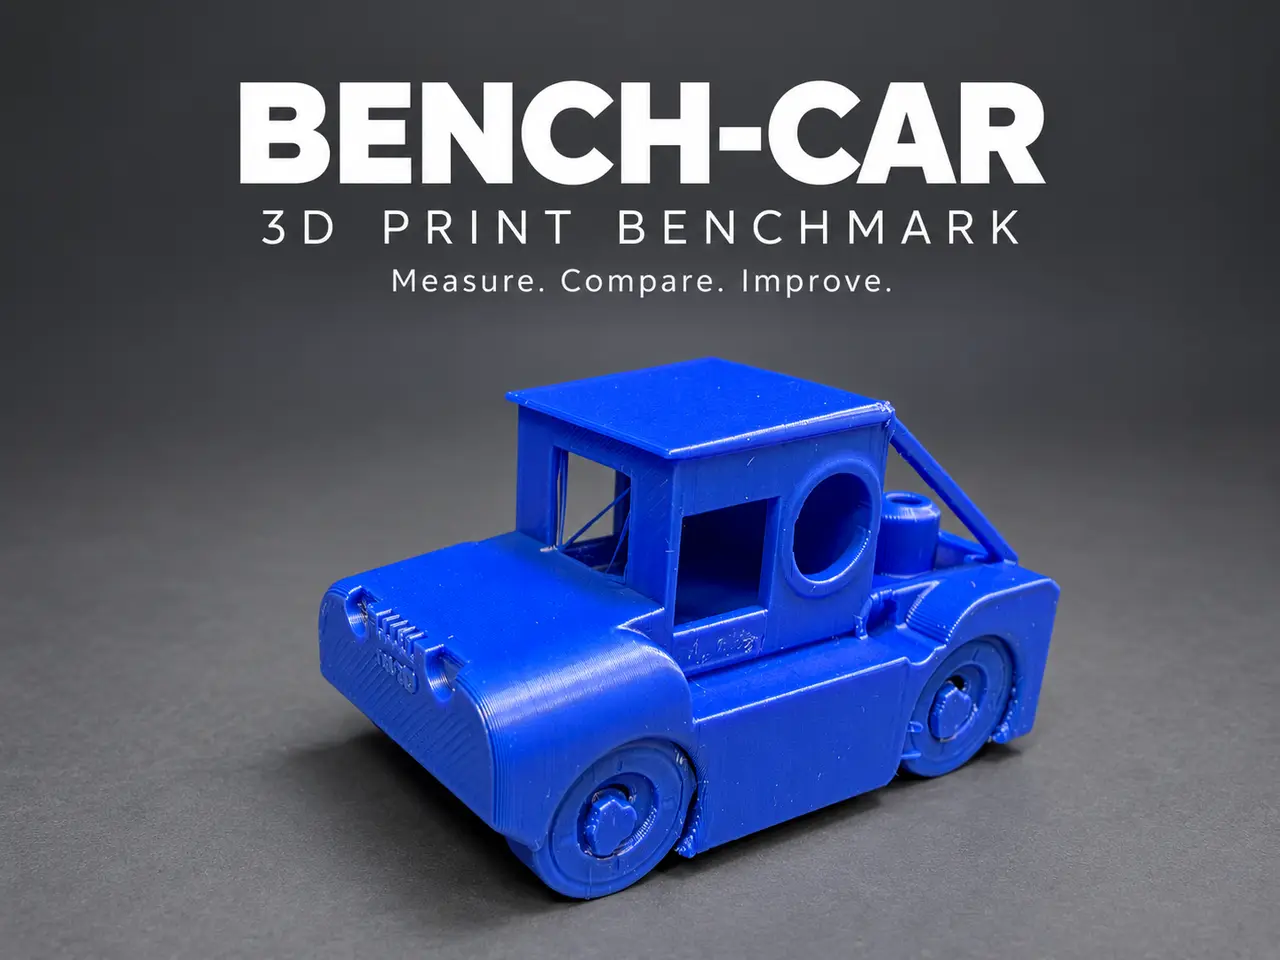
Print-in-place benchmark car with moving wheels, measurement guide and original STEP/STL. Print rear-end down.
Licencia
Uso comercial permitidoPuedes imprimirlo, modificarlo y venderlo sin pedir permiso ni dar crédito.
Al descargar aceptas respetar la licencia y dar crédito a JAV3D.
Archivos (5)
- Categoría
- Para tu impresora
- Formatos
- STEP, 3MF, STL, CSV, TXT
- Descargas
- 0
- Publicado
Sobre este modelo
Bench-Car – Print-in-Place 3D Printer Benchmark A small car with a practical job: compare surface finish, fine detail, circular openings, clearances and dimensional accuracy, then free the wheels and let it roll. Bench-Car combines visible test features with a compact, recognizable shape. The real blue print is shown in the gallery. Original STEP and STL files are included alongside the platform-specific 3MF project. PRINT ORIENTATION — IMPORTANT Print standing vertically on the flat rear end, with the front/grille pointing upward, exactly as stored in the supplied 3MF. The wheels are vertical and the vehicle's length becomes the build height, about 60 mm. The photos showing the car on its wheels are display views, not the supplied print orientation. Keep 100% scale for comparisons with the measurement guide. When importing STEP or STL, verify orientation and bed contact rather than assuming automatic placement is correct. The supplied profiles have supports disabled. Supports inside the wheel spaces can prevent the wheels from releasing and hide the clearances being tested. Check the sliced preview before printing. The vendor projects use auto brim; the PrusaSlicer project has brim width set to 0 mm. Inspect bed adhesion and keep any brim away from moving gaps. Record any change in orientation, support, brim, material or settings because it affects the comparison. AFTER PRINTING — FREE THE WHEELS Allow the print and build plate to cool, then remove the car and any brim. Hold the solid body, not the roof or thin braces. Gently wiggle each wheel back and forth to release it; the wheels can then rotate. Work gradually and do not force them. Remove loose strings or small burrs without widening the intended gaps. If a wheel remains fused, inspect the sliced gap and extrusion/first-layer quality before trying again. No separate screws, axles or purchased hardware are required for the wheel-release operation. WHAT TO INSPECT • Wheels and arches: roundness, surface finish and whether the printed clearances remain open. • Round and rectangular cabin openings: contour accuracy, small-feature definition and edge quality. • Roof, hood and body sides: consistent lines, seams, ringing, rough surfaces and local defects. • Inclined braces and narrow edges: complete extrusion, straightness and damage during removal. • Grille, lettering and wheel hubs: readable small details and grooves that remain distinct. • Open areas: stringing and travel marks. These are comparative observations. The model does not contain a calibrated series of overhang angles, bridge lengths or fit clearances. Which surfaces are overhangs or bridges depends on print orientation. It is not a temperature tower, maximum-flow test or mechanical strength certification. MEASUREMENT GUIDE — ORIGINAL GEOMETRY, NO ADDED MARKS Use the annotated English measurement image in this description. The car is shown on its wheels for easy identification of the measuring locations; print it on its rear end as described above. A — Wheelbase: 38.00 mm between the two axle centers on one side. B — Wheel outside diameter: 15.30 mm. Avoid raised hub details when measuring. C — Round cabin window: 9.00 mm nominal diameter. Check in two directions with suitable internal measuring tools or gauge pins. D — Small side bore below the cabin: 4.00 mm nominal diameter. E — Wheel-arch clearance: 0.60 mm radially, calculated from an 8.25 mm arch radius minus a 7.65 mm wheel radius. This is not axle clearance or an all-around minimum gap. F/G — Roof, window edges and inclined braces: inspect finish, straightness and feature completeness. H — Flat body width: 31.00 mm, measured between the plain body sides, avoiding lettering and protrusions. The complete CAD envelope, including tiny details, is approximately 60.065 × 31.017 × 36.650 mm in the normal vehicle length/width/height order. In the supplied print orientation, the approximately 60 mm vehicle length is vertical. Measure only after cooling. Repeat measurements and avoid flexible or rough edges. Record error as measured dimension minus nominal dimension; percentage error = error / nominal × 100. Compare prints using the same material, orientation, scale and measuring method. On a rear-end-up print, the 38 mm wheelbase is a build-Z measurement. A single discrepancy does not by itself identify the cause: measurement technique, material shrinkage, first-layer expansion and extrusion settings can all matter. FILES AND PROFILE NOTES Original Bench-Car.step and Bench-Car.stl are provided for editing and use in other slicers. Use the 3MF intended for your slicer and printer, then verify printer, nozzle, material, bed temperature and preview. Stored presets are not evidence that every listed printer/material combination has been physically tested. • Bambu Studio: H2D, 0.4 mm nozzle, 0.12 mm layers, 0.20 mm initial layer, 2 walls, 15% gyroid, supports off, PLA assigned to the model. • Creality Print: Creality Hi, 0.4 mm nozzle, 0.16 mm layers, 0.20 mm initial layer, 2 walls, 15% grid, supports off, PLA assigned to the model. • Anycubic Slicer Next: Kobra S1, 0.4 mm nozzle, 0.16 mm layers, 0.20 mm initial layer, 2 walls, 15% grid, supports off, PLA assigned to the model. • Elegoo Slicer: Centauri Carbon, 0.4 mm nozzle, 0.16 mm layers, 0.20 mm initial layer, 2 walls, 15% rectilinear, supports off. The supplied file assigns ABS; choose the correct material preset for your actual spool before slicing. Do not print PLA with an ABS preset. PrusaSlicer project: Prusa CORE One HF 0.4 mm nozzle, PLA, 0.20 mm layers and initial layer, 2 perimeters, 15% grid, supports disabled. Check the actual printer preset before slicing. Only the project for the relevant platform is included as its main print profile; the original geometry and guide remain common. The gallery documents the creator's physical blue print, not validation of every converted profile. The cover is based on a real print photo with an AI-edited background and English promotional text. The unedited gallery photos show the print's actual finish and imperfections. PUBLIC DOMAIN Released as Public Domain / CC0 where supported. You may print, share, adapt and use the model commercially under the selected public-domain dedication. The original geometry has not been modified for the measurement illustration. Measurement guide — nominal dimensions on the original model:
Print orientation: stand the car on its flat rear end, with the front pointing upward.
Descripción original del autor, publicada en Printables.